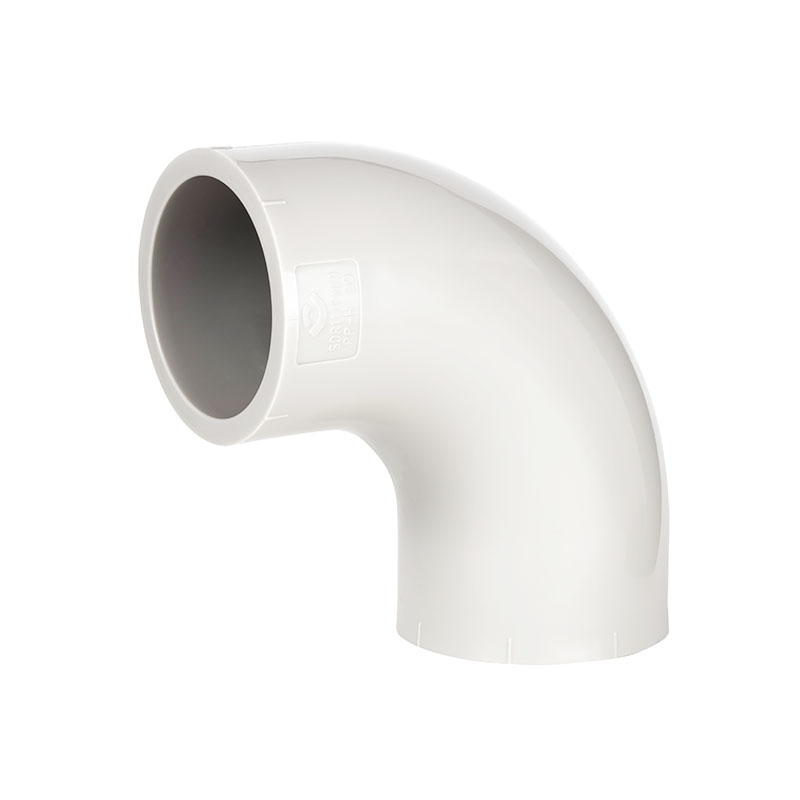
WXHENGDA supplies PPH Pipes Products and Valves .PPH Products. Complete sizes from 1/2" to 16". High quality with best wholesale prices. For more details about our PPH Products, please contact us!
Multi-Scenario Adaptability: Core Applications of PPH Products
PPH Products, with their stable physical properties and chemical resistance, have become a preferred solution for piping systems across multiple industries, serving a wide range of applications:
1. Industrial Processing
Chemical & Pharmaceutical Plants: Ideal for conveying corrosive media including hydrochloric acid (≤30%), sulfuric acid (≤50%), sodium hydroxide (≤40%), and organic solvents (e.g., ethanol, acetone). Resists chemical erosion at temperatures up to 95℃, ensuring long-term stability in harsh environments.
Food & Beverage Industry: Meets FDA 21 CFR Part 177.1520 food contact standards. Used for transporting pure water, fruit juices, dairy products, and syrup—non-toxic, odorless, and easy to clean, avoiding cross-contamination.
2. Municipal Infrastructure
Water Treatment Systems: Suitable for municipal sewage treatment, industrial wastewater recycling, and desalination projects. The smooth inner wall (roughness coefficient ≤0.01) prevents sediment accumulation, reducing maintenance frequency.
Heating & Cooling Networks: Withstands continuous operating temperatures of 70-90℃ (short-term peak up to 110℃) and low temperatures of -20℃ without embrittlement. Widely used in residential district underfloor heating and factory cooling water pipelines.
3. Specialized Fields
Renewable Energy: Serves as cooling pipes in solar thermal power plants and hydrogen fuel cell systems, resistant to high-temperature steam and hydrogen permeation.
Mining Industry: Conveys mineral slurries and acidic mine drainage, replacing traditional steel pipes to avoid rust and reduce replacement costs by 40% annually.